Pressure Washing Outdoor Furniture: PSI Limits and Coating Safety
2026-10-29 · 7 min read · By AOTUDE Furniture Team
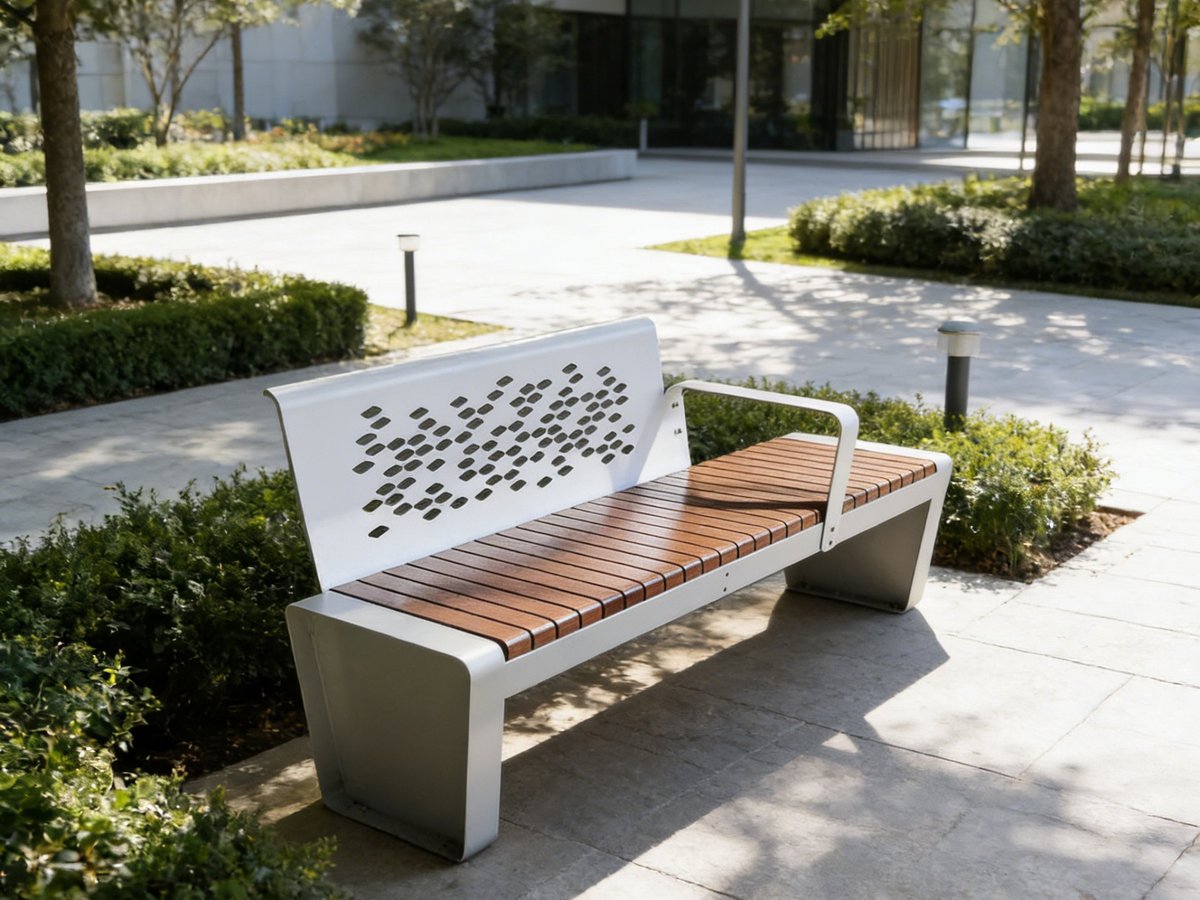
Every spring, municipal grounds teams and landscape contractors face the same backlog: a winter's worth of road salt, tyre spray, algae, bird droppings and chewing gum sitting on benches, bins and planters. Pressure washing outdoor furniture is the fastest way to clear it - and the fastest way to destroy a factory finish if the machine is set up for concrete rather than coated steel. A 4,000 PSI lance held 100 mm from a powder-coated seat rail will strip coating, open seams and drive water into a hollow section that then rusts from the inside. This guide sets out workable pressure ranges by material, the nozzle and standoff technique that keeps coatings intact, what pressure washing genuinely cannot fix, and the drying and post-wash checks that determine whether the clean buys you five more years of asset life or a repaint bill.
Why Deep Cleaning Belongs in the Asset Plan, Not the Complaint Log
Cosmetic soiling has a maintenance cost curve. Algae and moss hold moisture against timber and coating edges, accelerating the exact failure mode - moisture ingress under a film - that shortens service life. Bird droppings are acidic and etch polyester powder within weeks. Road salt left in crevices keeps driving galvanic activity on fasteners long after the last gritting run. Deferred cleaning therefore converts a low-cost wash into coating repair, slat replacement and, eventually, early asset replacement.
The practical rule most parks departments converge on: one deep clean per year in the shoulder season, doubled in coastal or high-footfall locations. That schedule fits the seasonal cycle described in our annual maintenance checklist, and it keeps the heavy equipment visit shared with paving and façade cleaning.
Pressure Ranges by Surface
The table below is a starting point for a cold-water machine with an adjustable unloader. Always test on a hidden face - the underside of a seat, the back of a bin panel - before committing to a full run.
| Surface | Working pressure | Nozzle | Standoff | Main risk if exceeded |
|---|---|---|---|---|
| Polyester powder-coated steel | 800-1,200 PSI (55-80 bar) | 25° or 40° fan | 300-500 mm | Chipping at edges, welds and fixing holes; water forced under the film |
| Hot-dip galvanised steel (uncoated) | 1,000-1,500 PSI | 25° fan | 300 mm | Scarring fresh zinc; no benefit on white storage stain |
| Brushed or satin stainless steel | 800-1,200 PSI | 40° fan | 400 mm | Directional scratch pattern; tea staining returns if rinse is skipped |
| Hardwood and modified timber slats | 600-1,000 PSI | 40° fan, wide | 400-500 mm | Raised grain, furring, leached oil, split end grain |
| GFRC and cast concrete planters | 1,500-2,500 PSI | 25° fan | 200-300 mm | Eroded face mix, damaged sealant joints, exposed fibre |
| Recycled polymer and WPC | 800-1,200 PSI | 40° fan | 400 mm | Surface scorching and colour fade |
Two settings matter as much as pressure: water temperature and chemical dose. Keep water below about 40 °C on coated steel so thermal shock does not craze the film, and never exceed the detergent dilution on the label - alkaline concentrates strip wax and dull satin stainless.
Nozzle Choice and Technique
Most coating damage attributed to "pressure washing" is actually nozzle and distance damage. A 0° pencil jet concentrates the entire pump output into a few square millimetres; at 200 mm it will cut through powder coating. Use a 25° fan for masonry and heavy soiling, a 40° fan for anything coated, and keep the lance moving at a steady 300-500 mm standoff with the fan angled slightly downwards so debris is pushed off the surface rather than into joints.
Technique details that make a measurable difference:
- Work top-down on vertical faces, then rinse bottom-up so dirty water does not streak clean panels.
- Stay off edges, weld toes and fixing holes - coating is thinnest there and water finds the gap first.
- Never direct the jet into drainage slots, vent louvres or hollow sections; a litre of trapped water inside a leg is a corrosion cell.
- Keep the fan off timber end grain and off any sealant bead around planter bases.
- Two passes at moderate pressure beat one pass at maximum for organic growth and salt film.
What Pressure Washing Cannot Fix
Pressure alone removes loose soil, not chemistry. Three common problems need a different method:
- Chewing gum. Cold gum smears under a jet. Steam (around 140-160 °C at the nozzle) or cryogenic freezing lifts it cleanly from paving and from bench feet; scraping afterwards risks scratching coated steel.
- Algae, moss and lichen. These need a biocide dwell time, not pressure. Beware chlorine: sodium hypochlorite is effective on masonry but attacks zinc and promotes chloride pitting on stainless steel, so use an oxygen-based or alkaline detergent on metal furniture and rinse thoroughly.
- Rust bloom and coating failure. Once red rust is visible at a weld or scratch, washing only reveals how far it has spread. That area needs mechanical preparation and a coating repair, following the field methods in our powder coating touch-up guide.
Graffiti sits in its own category: solvent choice and dwell time dominate, and pressure washing after solvent removal is mainly a rinse step. Our graffiti removal guide covers the surface-by-surface sequence.
Wash-Water, Runoff and Site Compliance
In many jurisdictions, wash water from public realm cleaning is trade effluent, not stormwater. Plan for it before the machine arrives: berm or block gully gratings, collect with a wet vacuum or portable sump, and discharge to foul sewer under the local consent. Detergents, oil and heavy metals from brake dust all travel with the runoff, and a visible suds trail into a watercourse is the kind of incident that ends a maintenance contract.
Practical controls: pH of discharge typically within 6-9, no visible foam, silt filtered before discharge, and a signed record of volumes for larger sites. On heritage or high-visibility paving, sheet the adjacent surface and work in 20 m sections so a single mistake stays contained.
The Four-Step Deep Clean
Use the same sequence every cycle so results are comparable year to year:
- Dry survey and pre-treat. Photograph pre-existing damage first - it protects you from damage claims and flags coating failures for repair. Pre-treat organic growth with biocide and allow the label dwell time.
- Loose debris and dry brushing. Clear grit from slat gaps and bin apertures so the jet does not pack it deeper.
- Wash by material zone. Group assets by substrate rather than by location, and change nozzle and pressure once per zone instead of repeatedly.
- Rinse, dry, inspect, record. Fresh-water rinse to remove detergent residue, 48-72 hours of drying before any timber re-oil, then a fastener and coating inspection with the results logged against the asset ID.
Post-Wash Care That Protects the Investment
Washing resets the clock only if the follow-up happens. Re-oil hardwood slats once the moisture content has stabilised, typically two to three days after washing in dry weather. Check anchor bolts and through-fixings for the loosening that a winter of freeze-thaw and vibration produces, and re-torque to the manufacturer's figure. Confirm drain holes in tubular legs and bin posts are clear - the wash is the best opportunity you will get to inspect them. On stainless, a plain water rinse within the same visit prevents the tea staining that chlorides leave behind.
Sourcing Furniture That Survives Annual Washing
Coating performance under repeated washing is decided at the factory, not on site. AOTUDE manufactures in Foshan at a 20,000 m² plant and sells direct, so the specification conversation is with the people who run the line: polyester powder over hot-dip galvanised steel where the environment demands it, coating thickness stated on the purchase order, sealed tube ends with drainage, and mechanical fixings instead of spot-welded joints wherever a component may need attention later. Per-model MOQ starts from 5 pcs, most models at 20 pcs, and custom or OEM runs from 50 pcs, with 5-10 year warranties against structural and coating defects. Browse the park bench range for powder-coated and galvanised platforms such as the Metro steel bench, or send drawings for an OEM/ODM quotation at aotude.com.